
7 Best Industrial Machine Vision Cameras for 2027
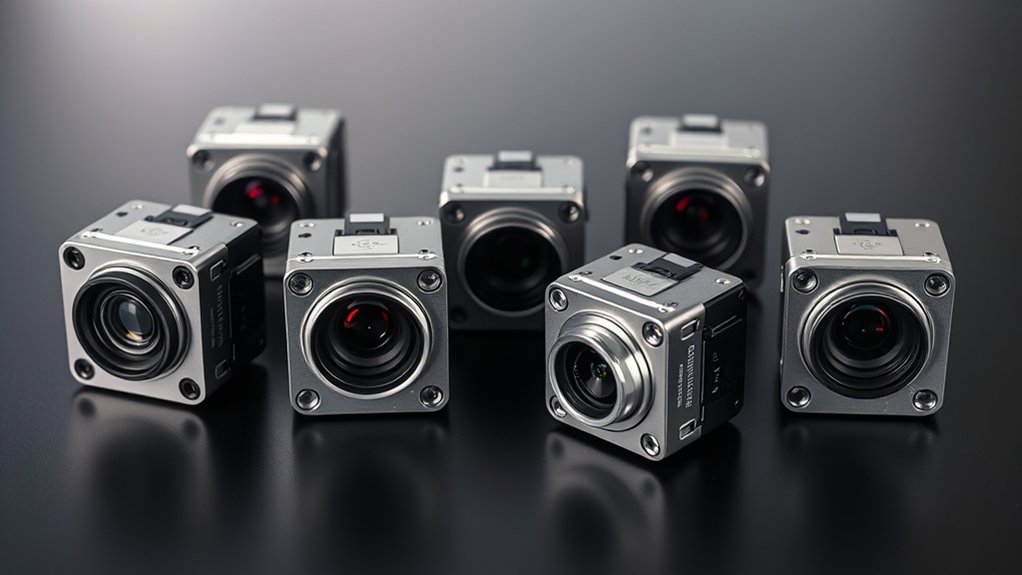
You’ll want cameras offering global shutter tech to capture sharp, motion-free images at high speeds. That’s essential for industrial machine vision cameras designed for fast inspections. For example, the USB3.0 4.0MP model excels with up to 88 fps, making it perfect for quick, precise work.
Basler’s 5MP GigE camera simplifies wiring through PoE, which is a real plus in complex setups. If you need detailed quality control, a rugged 21MP camera is your go-to. It handles fine details like a pro but requires high data capacity.
For varied tasks and lighting conditions, compact 2MP monochrome and color models are great choices. They offer flexibility without sacrificing quality. Keep following to discover which features best match your application needs!
| Image | Name | Editor's Rating | Price |
|---|---|---|---|

|
|
||

|
|
||

|
|
||

|
|
||

|
|
USB3.0 4.0MP Machine Vision Industrial Camera Global Shutter Monochrome
- 1) Camera transfer speed is fast.
- 2) Provide SDK, easy to use and convenient.
- 3) Support external trigger and flash.
Experience precise imaging like never before with the USB3.0 4.0MP Machine Vision Industrial Camera. Designed for demanding industrial environments, this camera delivers crisp, distortion-free monochrome images with its global shutter CMOS sensor. Its 2048 × 2048 resolution ensures every detail is captured accurately.
This camera excels at capturing fast-moving objects, shooting continuously at up to 88 frames per second. Whether you need manual control over focus and exposure or prefer automatic settings, it adapts seamlessly to your workflow. The USB 3.0 interface ensures rapid data transfer, minimizing delays in image processing.
Its compact and lightweight design, weighing just 2.4 ounces, makes integration into tight spaces effortless. The camera supports external triggers and flashes, adding versatility to complex inspection systems. Maintenance is straightforward, with durable construction suited for controlled indoor environments.
Best for: Industrial and scientific professionals requiring high-speed, accurate monochrome imaging for machine vision and video inspection applications.
What We Like:
- Sharp 4.0 MP global shutter sensor for distortion-free images
- High-speed capture at 88 frames per second for moving targets
- Versatile SDK support for Windows and Linux integration
- Compact, lightweight design for easy installation
Specification:
| Feature | Details |
|---|---|
| Manufacturer | Not specified |
| Resolution | 2048 × 2048 pixels |
| Sensor Type | Global shutter CMOS |
| Frame Rate | Up to 88 fps |
| Interface | USB 3.0 |
| Weight | 2.4 ounces (68 grams) |
| Color | Monochrome |
Basler acA2500-20gm 5MP Monochrome GigE Camera
- High Resolution 5MP Monochrome Imaging: Delivers sharp 2592 x 2048 pixel images with the onsemi PYTHON 5000 CMOS sensor...
- Global Shutter Technology: Captures distortion-free images of fast-moving objects at up to 21 frames per second (full...
- GigE Vision with PoE Support: Gigabit Ethernet interface with Power over Ethernet (IEEE 802.3af) for simple single-cable...
The Basler acA2500-20gm is designed for users who need sharp, distortion-free images of fast-moving subjects. Its 5 MP monochrome sensor with a global shutter captures clear images without motion blur. This makes it ideal for capturing precise details in dynamic environments.
The camera offers programmable exposure, AOI, and pixel binning. These features allow you to customize image capture for specific tasks. Its GigE Vision interface supports Power over Ethernet, reducing cable clutter and simplifying setup.
Its compact and lightweight design fits easily into tight spaces. This makes it perfect for OEM integration and applications with limited room. Built to withstand 24/7 operation in harsh industrial settings, it ensures reliable performance over long periods.
Maintenance is straightforward due to its rugged construction. However, it only captures monochrome images and has a maximum frame rate of 21 fps, which may limit some ultra-high-speed applications. The operating temperature range is capped at 50°C, so it’s best used in controlled environments.
Best for: Industries and professionals needing high-speed, distortion-free monochrome imaging for machine vision, automation, and scientific research.
What We Like:
- Clear, distortion-free images with a 5 MP global shutter sensor
- Simplified installation with GigE Vision and Power over Ethernet
- Compact, lightweight design for easy integration in tight spaces
- Programmable exposure and pixel binning for tailored image capture
Specification:
| Feature | Details |
|---|---|
| Manufacturer | Basler |
| Resolution | 5 Megapixels (2592×2048) |
| Sensor Type | Monochrome CMOS |
| Shutter Type | Global Shutter |
| Max Frame Rate | 21 fps |
| Interface | GigE Vision (PoE) |
| Dimensions | Ultra-compact (specific size not provided) |
| Weight | Lightweight (exact weight not provided) |
| Operating Temperature | Up to 50°C |
Industrial Machine Vision Camera 21MP Global Shutter
- Model number: CA-HF2100M, industrial camera designed for industrial imaging applications.
- Compatible with industrial imaging systems requiring high-resolution capture for industrial use cases.
- Constructed with durable materials suitable for operation in industrial environments.
Experience precise imaging like never before with the 21MP global shutter industrial machine vision camera. Designed to capture fast-moving processes, it delivers sharp, high-resolution images that reveal critical details often missed by standard cameras. This precision helps reduce errors and improve quality control in complex manufacturing environments.
The CA-HF2100M supports continuous, stable operation, ensuring minimal downtime in demanding factory settings. Its robust construction withstands harsh conditions, while seamless integration with industrial automation systems simplifies installation and maintenance. This camera streamlines inspection workflows and enhances overall productivity.
With its global shutter technology, motion blur is eliminated, making it ideal for monitoring rapid machine movements. However, the high-resolution output requires sufficient data handling capabilities, and its specialized interfaces may limit use outside industrial contexts. Despite this, it remains a reliable solution for high-speed, detailed imaging needs.
Best for: Industrial manufacturers and automation engineers requiring precise, high-speed imaging for quality inspection and process monitoring in challenging factory environments.
What We Like:
- Captures sharp, blur-free 21MP images of fast-moving targets
- Built for continuous, reliable use in tough industrial conditions
- Easily integrates with existing machine vision and automation systems
- Durable design ensures stable performance over long periods
Specification:
| Feature | Details |
|---|---|
| Manufacturer | CA-HF Series |
| Resolution | 21 Megapixels |
| Shutter Type | Global Shutter |
| Operation | Continuous Industrial Use |
| Integration | Industrial automation compatible |
| Construction | Rugged, durable housing |
Industrial 2MP Monochrome Machine Vision Camera
- Model number: CA-H200M, featuring a 2MP monochrome sensor for industrial imaging applications.
- Equipped with a 16x speed CMOS sensor to support fast image capture and processing tasks.
- Includes a C-mount lens mount for compatibility with a range of compatible lens accessories.
Experience precise industrial inspections with the CA-H200M, a fast and reliable 2MP monochrome machine vision camera. Its high-speed 16x CMOS sensor captures sharp images quickly, helping engineers detect defects and measure dimensions accurately. This efficiency reduces downtime and enhances quality control processes.
The camera’s durable design includes an IP64 rating, protecting it from dust and splashes in demanding industrial environments. Its compact size and manageable weight allow smooth integration into automated inspection lines. Maintenance is straightforward, ensuring consistent performance with minimal effort.
Designed with compatibility in mind, the CA-H200M supports standard C-mount lenses, making it easy to fit into existing machine vision setups. While its monochrome sensor specializes in black-and-white imaging, it excels in applications where color is unnecessary.
Though weighing 6.6 pounds and measuring 11.81 inches cubed, it balances robustness with practicality. This camera is ideal for environments where reliability and image precision are critical.
Best for: Engineers and quality control specialists seeking a dependable 2MP monochrome camera optimized for industrial inspection and machine vision tasks.
What We Like:
- Fast 16x CMOS sensor for quick, accurate image capture
- IP64 rating ensures protection against dust and splashes
- Compatible with standard C-mount lenses for easy system integration
- Compact and sturdy design suited for automated inspection lines
Specification:
| Feature | Details |
|---|---|
| Manufacturer | Feikteey |
| Dimensions | 11.81 in³ |
| Weight | 6.6 lb |
| Sensor Type | 2MP Monochrome CMOS |
| Lens Mount | C-mount |
| Protection Rating | IP64 |
Industrial Machine Vision Camera Color Sensor 2 Megapixel ANPVC1210
- The ANPVC1210 is a 2-megapixel color machine vision camera designed for industrial inspection and measurement...
- This industrial vision sensor features a compact and robust housing, constructed to withstand typical factory floor...
- Compatible with standard machine vision interfaces, the camera integrates easily with common industrial control and...
Experience precise color detection like never before with the ANPVC1210 industrial machine vision camera. This 2-megapixel color sensor delivers sharp, detailed images that enhance the accuracy of your inspections. It solves common challenges in quality control by clearly distinguishing hues and contrasts critical for assembly verification.
Designed for demanding factory environments, the ANPVC1210 features a compact, robust housing that endures continuous operation. Maintenance is straightforward, with easy adjustments for focus and exposure to adapt to varying lighting conditions. This ensures consistent image clarity without frequent recalibration.
The camera integrates smoothly with standard machine vision and industrial control systems, simplifying your setup and reducing downtime. Its design supports reliable, long-term use, making it a practical choice for manufacturers seeking dependable color-based inspection solutions.
While the camera’s weight of 6.6 pounds and its packaging size might restrict mounting options in tight spaces, its durability and imaging precision make these trade-offs manageable. The first availability in 2026 suggests planning ahead for integration into your production line.
Best for: industrial manufacturers and quality control teams needing precise color-based inspection and reliable imaging in demanding production environments.
What We Like:
- High-resolution 2-megapixel color sensor for accurate color differentiation
- Durable, compact housing built for continuous factory use
- Easy focus and exposure adjustments for varied lighting
- Seamless integration with standard machine vision systems
Specification:
| Feature | Details |
|---|---|
| Manufacturer | ASBLUE |
| Resolution | 2 Megapixels |
| Weight | 6.6 lb (3.0 kg) |
| Dimensions | 11.81-inch cube (30 cm³) |
| Color Sensor | Industrial-grade color |
Industrial Machine Vision Camera 2MP Gigabit Ethernet
- This industrial camera features a 2-megapixel CMOS sensor with a global shutter, designed for capturing clear images of...
- The camera provides high-resolution imaging with a fast frame rate over its Gigabit Ethernet (GigE) interface, enabling...
- Constructed for industrial environments, the KV-CL20 model is built with durable materials to withstand typical...
Capturing high-speed motion with accuracy is crucial in automated inspections. The Industrial Machine Vision Camera 2MP Gigabit Ethernet is designed to eliminate motion blur, ensuring clear images every time. Its 2MP CMOS sensor with a global shutter precisely captures fast-moving objects without distortion.
This camera supports real-time image processing thanks to its fast frame rate and low latency. The Gigabit Ethernet interface enables quick data transfer, allowing smooth integration with existing machine vision systems. Its compact and rugged build makes it resilient in harsh industrial environments.
Maintenance is straightforward since the camera requires a constant connection to external systems for image capture, as it lacks built-in media storage. This design choice helps keep the device compact and reliable for continuous operation. It’s ideal for tasks like assembly line monitoring, robotics, and automated quality control.
Best for: Industrial automation engineers and quality control professionals needing a reliable, fast vision camera for precise inspection in dynamic manufacturing settings.
What We Like:
- Clear, motion-free imaging with global shutter CMOS sensor
- High-speed data transfer via Gigabit Ethernet
- Durable, compact design suited for tough industrial use
Specification:
| Feature | Details |
|---|---|
| Manufacturer | ASBLUE |
| Resolution | 2 Megapixels |
| Sensor Type | CMOS with Global Shutter |
| Interface | Gigabit Ethernet |
| Dimensions | Compact (exact size not specified) |
| Weight | Not specified |
| Color Options | Not specified |
Industrial Machine Vision Camera Color Sensor 2 Megapixel ANPVC1210
- This ANPVC1210 machine vision sensor features a 2-megapixel color imaging array, delivering detailed, accurate visual...
- Designed for compatibility with standard industrial machine vision mounting hardware and control systems, this sensor...
- Constructed with heat-resistant, dust-proof industrial-grade housing, the ANPVC1210 withstands harsh manufacturing...
Experience reliable, high-quality color imaging with the ANPVC1210, designed to enhance industrial machine vision systems. This 2-megapixel sensor provides sharp visuals that improve real-time quality control and automated inspection processes. It helps reduce errors by delivering consistent frame rates and accurate image data for precise decision-making.
The camera’s robust design includes a heat-resistant, dust-proof housing, protecting it from typical industrial challenges like vibration and temperature changes. This ensures long-lasting performance with minimal maintenance, reducing downtime in demanding environments. Its compact build fits standard machine vision mounts, making integration straightforward.
Engineered for manufacturing, packaging, and assembly lines, the ANPVC1210 supports applications such as parts sorting and robotic guidance. It connects seamlessly to common control systems using industrial communication protocols, streamlining data transfer and simplifying system setup.
While the resolution suits most industrial inspection needs, users requiring ultra-high-definition imaging may find it limiting. Installation may require specific mounting hardware, and its environmental resistance is best suited for moderate industrial conditions.
Best for: Industrial manufacturers and automation engineers seeking dependable 2-megapixel color sensors for quality assurance and robotic applications.
What We Like:
- Delivers precise 2-megapixel color imaging with stable frame rates for accurate monitoring
- Durable housing protects against heat, dust, and vibrations
- Easy integration with standard mounts and industrial control systems
- Supports efficient automated quality control and sorting processes
Specification:
| Feature | Details |
|---|---|
| Manufacturer | ANPVC |
| Resolution | 2 Megapixel |
| Color Sensor | Yes |
| Housing | Heat-resistant, dust-proof |
| Mount Compatibility | Standard machine vision mounts |
| Communication | Industrial protocols |
| Typical Use | Industrial quality control, parts sorting, robotic guidance |
Factors to Consider When Choosing an Industrial Machine Vision Camera
When choosing an industrial machine vision camera, you’ll need to focus on resolution and sensor type to meet your image quality needs. Consider shutter mechanisms and frame rates to capture fast-moving objects accurately.
Don’t forget to check connectivity options and lens compatibility to guarantee seamless integration with your system. These details might seem small, but they make a big difference in how well everything works together.
Resolution and Sensor Type
Although you might prioritize resolution for detailed inspections, choosing the right sensor type is just as essential for achieving accurate results in industrial machine vision. Higher resolution sensors, ranging from 2 to 21 megapixels, let you capture finer details and larger fields of view but generate bigger files that demand more processing power and storage.
You’ll want to match effective resolution—that is, usable pixels like 2048×2048—to your required field of view and spatial resolution to reliably detect defects. Sensor pixel size plays a pivotal role: larger pixels gather more light, improving sensitivity and dynamic range, while smaller pixels boost resolution within the same sensor area.
Monochrome sensors offer higher sensitivity and contrast, which is ideal for many inspections. On the other hand, color sensors are necessary when color differences matter for defect detection. So, it really depends on what you need to spot in your inspection.
Shutter Mechanism Options
Since capturing crisp images of fast-moving objects is essential in industrial machine vision, choosing the right shutter mechanism can make all the difference. Global shutters capture the entire sensor simultaneously, eliminating rolling distortion and ensuring accurate measurements at high speeds.
They’re ideal for high-speed inspection, motion analysis, and robotics where precise geometry and timing matter. On the other hand, rolling shutters read out line-by-line, which can cause skew or wobble artifacts when imaging fast motion or strobe lighting.
However, rolling-shutter cameras often offer higher pixel counts or lower costs, making them suitable for static scenes or controlled lighting with slower movement. When selecting a shutter mechanism, weigh trade-offs like sensor availability, frame rate, noise performance, and budget to find the best fit for your application.
Frame Rate Performance
Capture every detail of fast-moving objects by prioritizing frame rate performance when choosing an industrial machine vision camera. Higher frame rates, often tens to hundreds of frames per second, help you avoid motion blur and improve inspection accuracy.
Make sure the camera’s continuous frame rate at your desired resolution meets your system’s throughput needs. Remember, frame rate usually drops as resolution or ROI size increases.
Choose a global shutter sensor to maintain image fidelity during fast motion. This helps avoid distortion that’s common with rolling shutters.
Also, think about data bandwidth and processing limits. Continuous high frame rates produce large data streams that can overwhelm interfaces like USB3.0 or GigE.
Finally, verify your camera supports precise triggering and synchronization. This keeps frame capture timing consistent, especially when using multiple cameras or automation systems.
Connectivity and Interface
How do you guarantee your industrial machine vision camera communicates effectively with your system? Start by selecting the right interface based on bandwidth needs—USB3.0 offers up to 5 Gbps, while Gigabit Ethernet provides about 1 Gbps per link and can scale higher with aggregation.
For long cable runs or distributed setups, Ethernet with Power over Ethernet (PoE) simplifies wiring by delivering data and power via a single cable. Makes things a lot neater and easier, right?
Make sure the camera supports protocols like GenICam or GigE Vision and matches your software environment for smooth integration. Also, check trigger, I/O, and GPIO options to handle hardware synchronization and external triggers.
Finally, consider latency, CPU load, and driver maturity, since these impact real-time performance and system responsiveness. These little details can make a big difference when your system is running live.
Lens Compatibility
After ensuring your camera communicates seamlessly with your system, the next step is to focus on lens compatibility. Start by choosing a camera with a standard lens mount like C-mount or CS-mount, so you can easily select and swap industrial lenses.
Make sure the lens’s image circle covers your sensor size—whether 2 MP, 5 MP, or 21 MP—to avoid vignetting and maintain your field of view.
Pick a focal length that suits your working distance and target size: short for wide scenes, long for detailed, distant inspections. Check the lens’s optical resolution (MTF) and aperture to match your camera’s pixel size and lighting.
This way, you’ll ensure crisp images with proper depth of field. Finally, confirm mechanical fit, including flange distance and thread type, to accommodate filters or protective elements.
Environmental Durability
When selecting an industrial machine vision camera, you’ll want to make certain it withstands the environmental conditions it will face on the job. Verify the camera’s ingress protection (IP) rating—IP64 or higher is ideal—to guard against dust and water spray.
Confirm its operating temperature range fits your setting. If you deal with extreme heat or cold, look for extended-temperature specs or heated housings.
Check vibration and shock ratings, like MIL-STD-810, especially if mounting on conveyors or mobile platforms. Also, make certain the housing resists corrosion, chemicals, and abrasion from cleaning.
Finally, opt for sealed connectors, cable strain relief, and conformal-coated PCBs to protect against moisture, oil, and condensation in harsh environments. These factors make certain reliable, long-lasting performance.
Software and SDK Support
Selecting an industrial machine vision camera means making certain its software and SDK support align with your development needs. Make sure the SDK offers APIs compatible with your preferred languages and frameworks like C++, Python, or OpenCV wrappers. This will speed up integration and help you avoid low-level coding.
Confirm support for standard protocols such as GenICam, GigE Vision, or USB3 Vision. This guarantees interoperability with third-party tools.
Check that the SDK provides sample code, documentation, and drivers for your target operating systems, including Windows or Linux. It really helps if everything is ready to go.
Also, verify advanced camera control support—triggering, GPIO, exposure settings, ROI, and hardware timestamping. These features enable precise capture and synchronization, which you’ll definitely want.
Finally, consider the vendor’s commitment to long-term SDK updates and technical support. It’s a smart move to reduce future integration risks.
Application-Specific Features
To zero in on the right industrial machine vision camera, you’ll need to weigh several application-specific features carefully. Start by choosing the resolution and sensor type that fit your inspection needs—consider defect size and field-of-view.
Match frame rate and exposure control to object speed to avoid motion blur. Decide between monochrome or color sensors based on whether you need intensity or color contrast.
Check that the camera’s interface and triggering options, like USB3.0 or GigE, meet your data bandwidth and synchronization requirements. Finally, make certain the camera’s mechanical and environmental specs, including lens mount, housing, ingress protection, and operating temperature, suit your system and factory conditions.
Addressing these factors guarantees reliable, precise vision performance tailored to your application. It’s all about making sure your camera fits just right for what you need.
Frequently Asked Questions
How Do Industrial Vision Cameras Integrate With AI Systems?
You connect industrial vision cameras to AI systems by feeding captured images into AI algorithms for real-time analysis. This enables automated defect detection, quality control, and decision-making.
It’s a great way to boost your production efficiency and accuracy markedly. Plus, it helps catch issues early, so you save time and resources down the line.
What Maintenance Is Required for Industrial Machine Vision Cameras?
You’ll need to regularly clean lenses, check connections, update firmware, and calibrate sensors to guarantee accuracy.
Also, inspect for physical damage and maintain proper environmental conditions to keep your industrial vision cameras running smoothly and reliably.
Keeping an eye on these things might seem like a lot, but it really helps avoid bigger problems down the line. Just a little regular care goes a long way!
Are There Wireless Options for Industrial Machine Vision Cameras?
Yes, you’ll find wireless industrial machine vision cameras that work like a well-trained guide, seamlessly transmitting data without cables. They offer flexibility and ease.
But you’ll want to weigh range, interference, and power requirements carefully. These factors can impact performance, so it’s worth considering them before making a choice.
How Do Lighting Conditions Affect Camera Performance?
Lighting conditions directly impact your camera’s image clarity and accuracy. Poor or inconsistent lighting can cause shadows, glare, or noise.
What Are the Common Software Platforms for Vision Camera Analytics?
Back in the days of floppy disks, you’d rely on software like Halcon, Cognex VisionPro, and OpenCV for vision analytics. Today, you’ll use these platforms because they’re powerful, flexible, and integrate seamlessly with your vision cameras.
They’ve really stood the test of time. Plus, they keep evolving to meet modern needs. So, whether you’re working on a simple project or something complex, these tools have got your back.
Conclusion
When choosing an industrial machine vision camera, remember that over 60% of manufacturers see improved quality control as their top benefit. You want a camera that fits your specific needs—whether it’s resolution, speed, or connectivity.
Keep in mind factors like sensor type and interface to guarantee you get the best performance. With the right choice, you’ll boost efficiency and accuracy, making your operations run smoother and smarter.
Picking the right industrial machine vision camera means considering what matters most to your setup. Whether it’s high resolution for detailed inspections, fast frame rates for quick processing, or reliable connectivity for seamless integration, these elements are key. Paying attention to sensor types and interfaces ensures your camera works perfectly with your system, helping you achieve better quality control and operational efficiency. In the end, the right machine vision camera can transform your production line by enhancing accuracy, speeding up processes, and reducing errors—making your industrial operations more productive and future-ready.